The global demand for high-efficiency ventilation systems has reached an unprecedented scale. Modern factories, automated warehouses, cloud computing data centers, and advanced agricultural structures depend heavily on industrial fan systems to manage high thermal output and maintain environmental equilibrium. The global industrial fan market is valued at billions of dollars, driven primarily by strict carbon neutrality requirements, occupational health standards, and the rapid growth of large-scale infrastructure projects across North America, Europe, and the Asia-Pacific region.
Today's top China industrial fan factories are moving away from simple mechanical ventilation. Instead, they are integrating energy-saving intelligent power controllers (PCBA), Variable Frequency Drives (VFDs), and IoT networks that sync with factory energy management systems (EMS). This industrial transition shifts focus from simple airflow generation to precise motor speed management, real-time thermal sensing, and predictive maintenance capabilities.
Modern industrial fans rely on advanced variable frequency drives (VFD) and intelligent power supply assemblies to scale performance dynamically, reducing energy consumption by up to 50% under variable loads.
With onboard computing units, ventilation systems run analytics locally to prevent motor failures, optimize blade speed based on environmental data, and send telemetric updates back to monitoring systems.
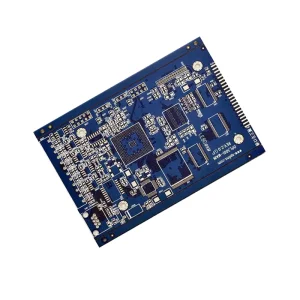
Industrial components demand extreme thermal and mechanical reliability. Our focus on immersion silver PCBs, HASL lead-free boards, and heat sink designs guarantees stable performance in harsh conditions.
Three main technology paths are defining the next generation of industrial ventilation:
Modern industrial fans require robust control systems to ensure reliability in challenging settings. Dust, chemical vapors, extreme temperatures, and electromagnetic interference (EMI) from heavy machinery can disrupt standard consumer electronics. To maintain performance, industrial ventilation relies on industrial-grade electronics, hardware controls, and reliable memory components.
This is where Vorynex Memory Technology supports the industrial chain. While top China industrial fan manufacturers focus on aerodynamics, blade structures, and casing engineering, Vorynex provides the high-performance memory infrastructure, computing modules, and PCB assemblies that power the control units of these industrial air management systems.
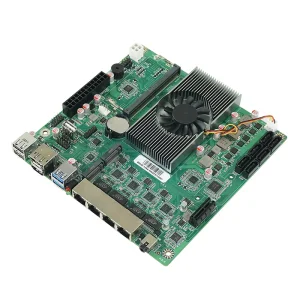
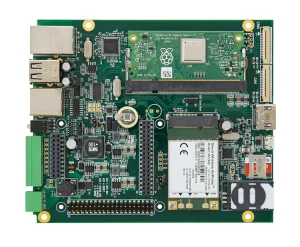
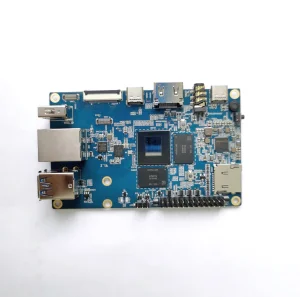
For smart ventilation towers, server room exhaust arrays, and factory HVAC systems, the central controller must process real-time sensor data and adjust system settings. To handle these demands, system developers use platforms like the Rockchip RK3588S Motherboard, which features a built-in NPU for AI edge computing, or the Raspberry Pi Industrial Control Board PCBA. These systems run software to adjust fan speeds based on real-time factors like humidity and particulate matter.
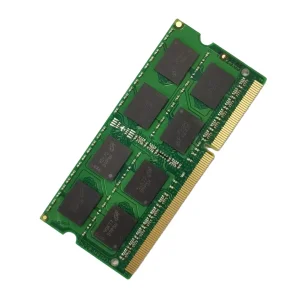
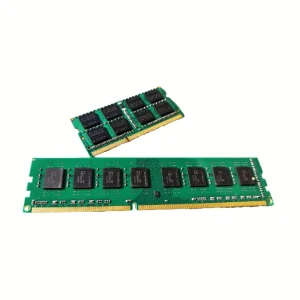
To run these applications smoothly and ensure reliable operation, the system requires high-quality memory modules. A single memory error can cause system downtime. Using specialized solutions, such as DDR4 ECC Memory modules, allows the controller to detect and correct single-bit data corruption, helping to ensure uninterrupted operations.
Vorynex Memory Technology (China) Co., Ltd. is a professional DDR5 memory manufacturer and OEM/ODM solution provider specializing in high-performance memory modules for global markets.
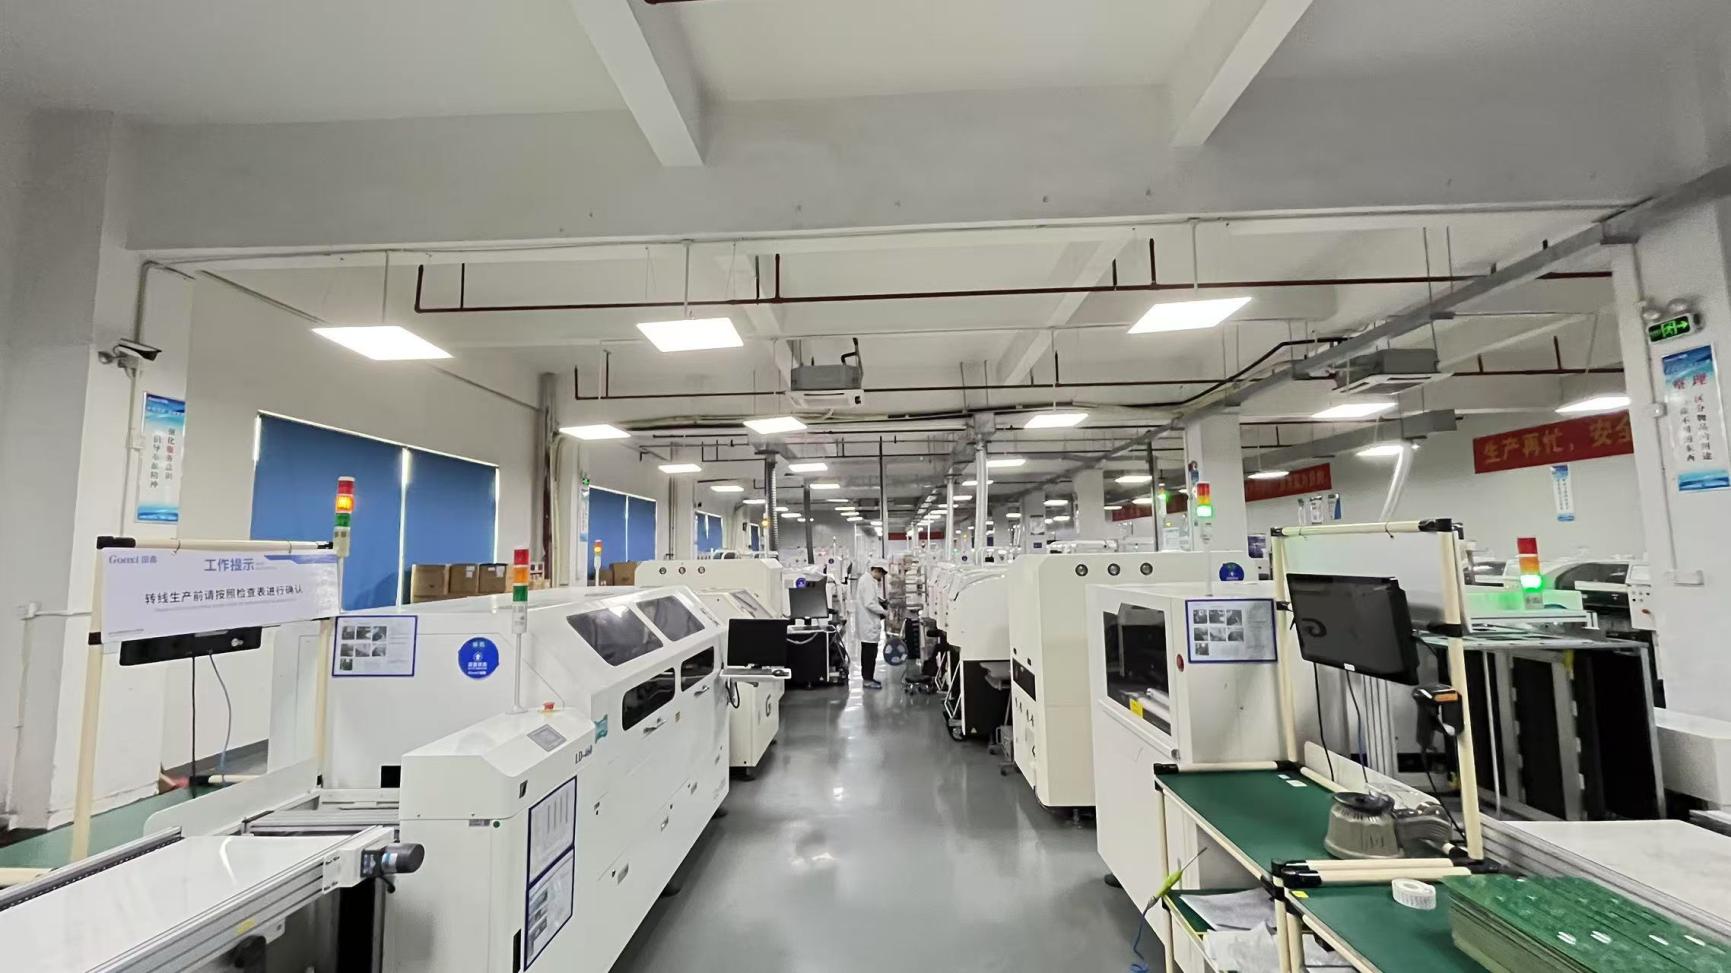
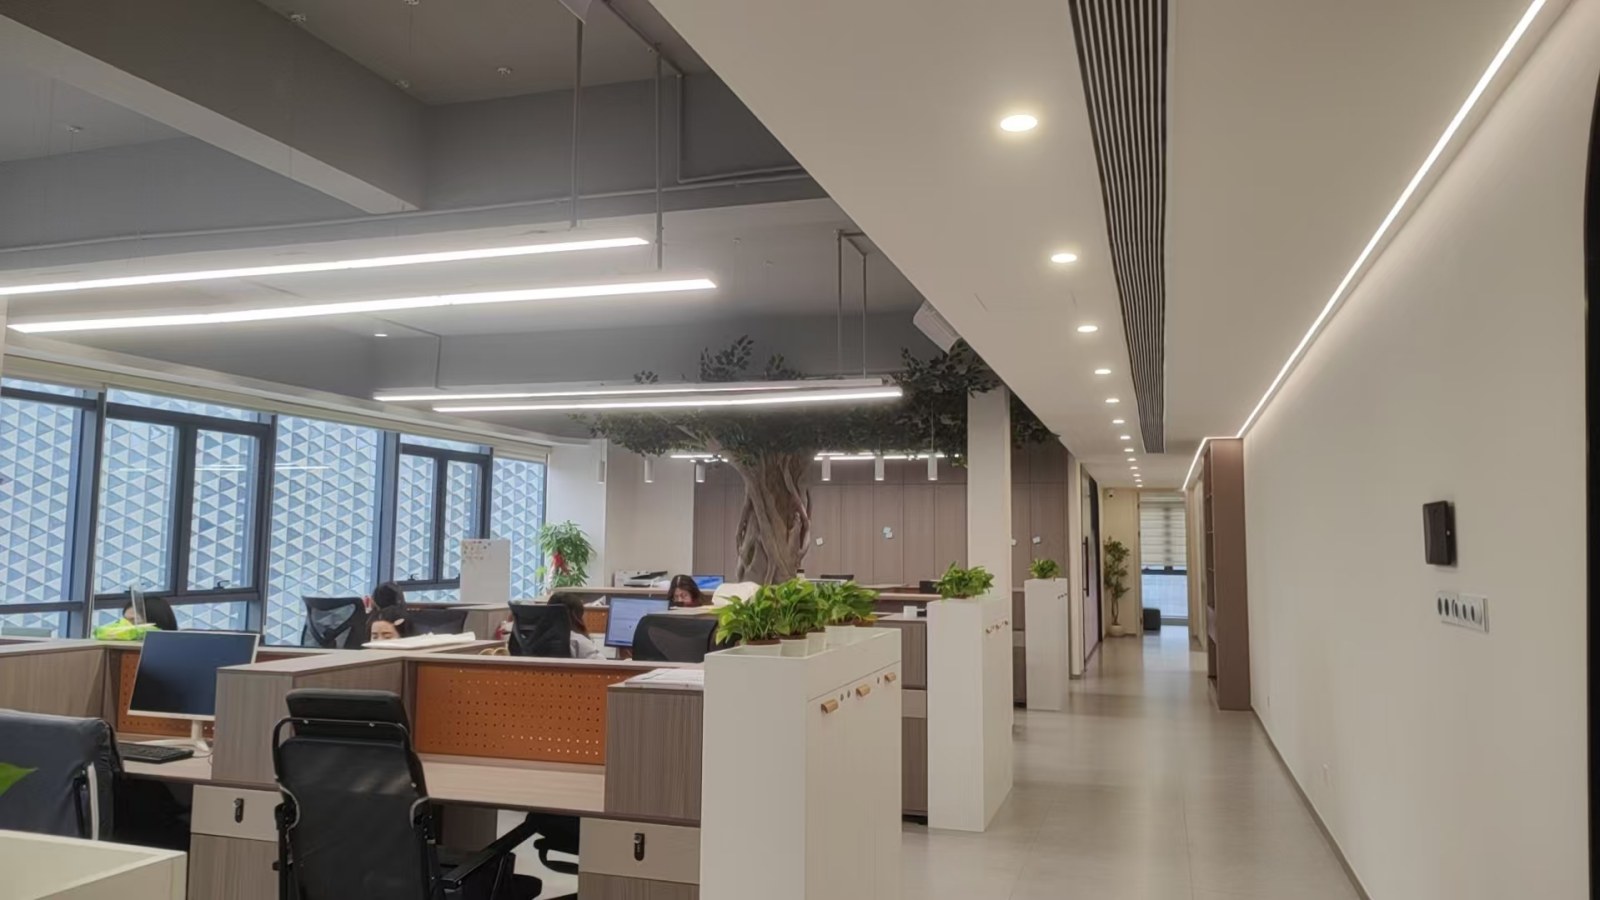
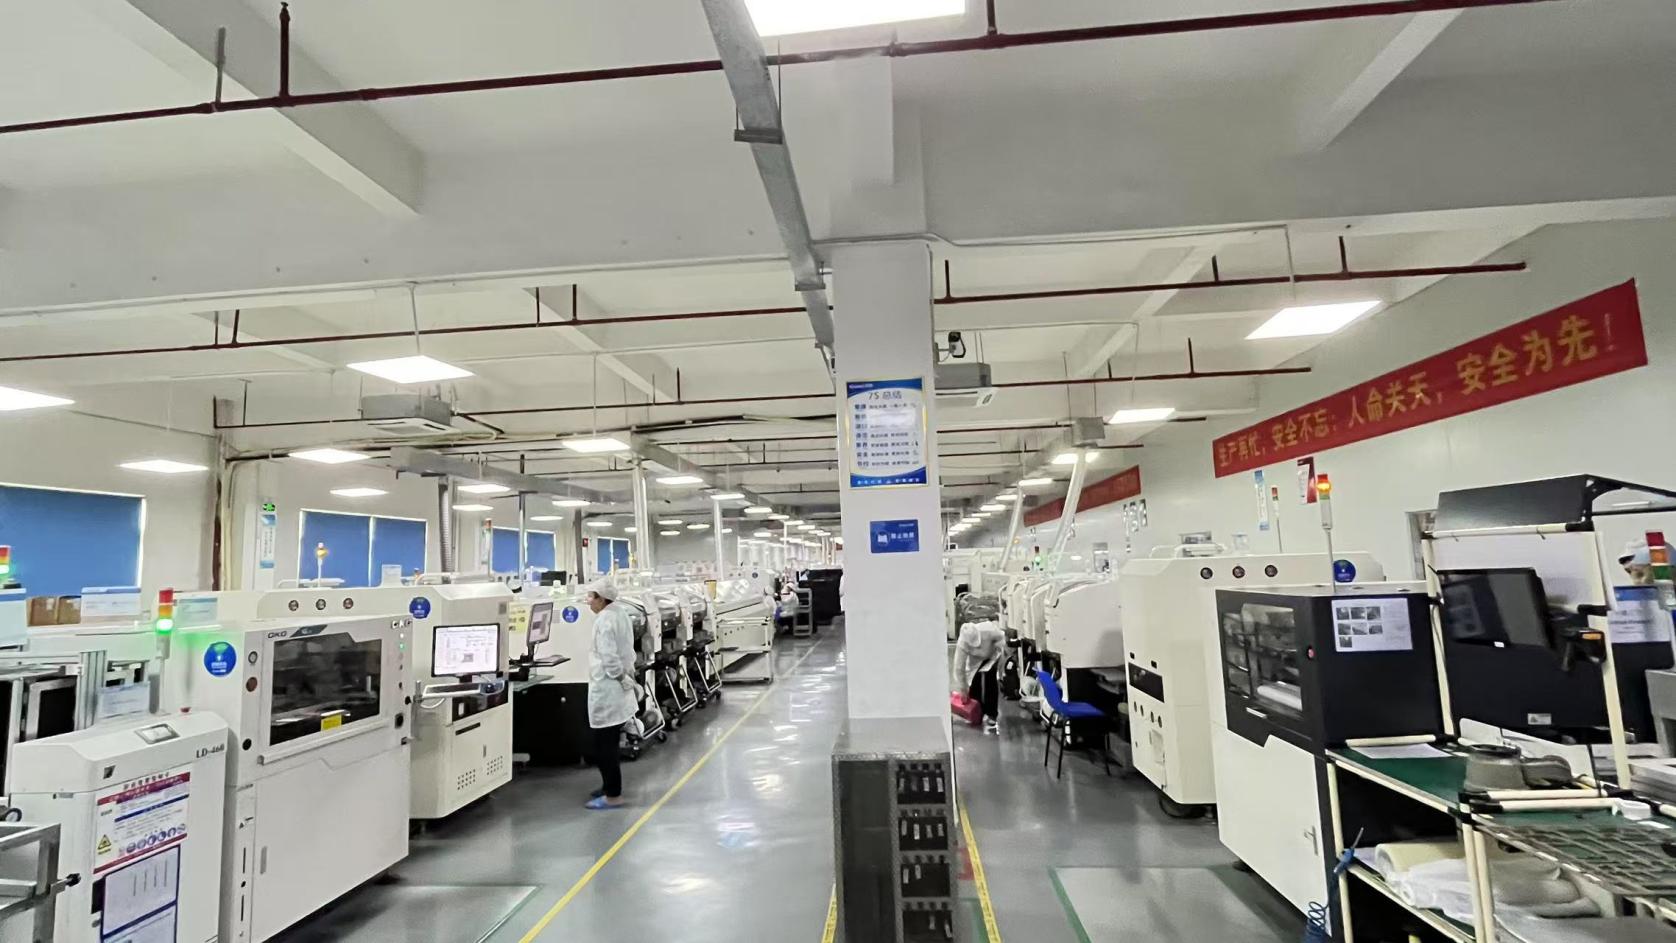
Established in 2016, the company has developed strong manufacturing and engineering capabilities over the years. With a modern production facility covering approximately 320㎡, Vorynex focuses on delivering stable, high-speed, and energy-efficient memory solutions for gaming, industrial, and enterprise applications.
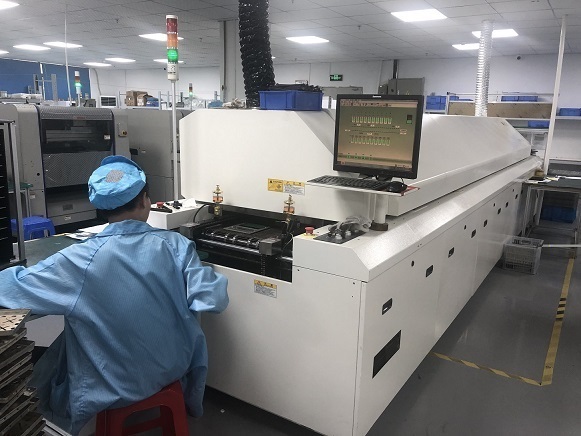
Vorynex maintains strict quality control standards, including 100% functional testing, aging tests, compatibility testing, and high-temperature stress testing. Product inspection methods include automated optical inspection (AOI), in-circuit testing (ICT), and final system-level validation. The quality assurance team consists of approximately 45 professional QC staff ensuring consistent product reliability.
With a strong international trade background, Vorynex serves key markets including North America, Europe, Southeast Asia, the Middle East, and South America. The company collaborates with more than 1,200 supply chain partners, enabling stable sourcing of high-quality DRAM chips and components.
Its primary customer base includes brand distributors, system integrators, industrial equipment manufacturers, and gaming hardware companies. Vorynex also has strong R&D capabilities, supported by a team of approximately 180 R&D engineers, focusing on memory architecture optimization, compatibility enhancement, and thermal performance improvement.
Customization is fully supported, including frequency tuning, PCB design customization, heat sink design, branding (private label), and firmware optimization. In the past year, the company successfully launched around 240 new product models, covering DDR4, DDR5, and specialized industrial memory solutions.
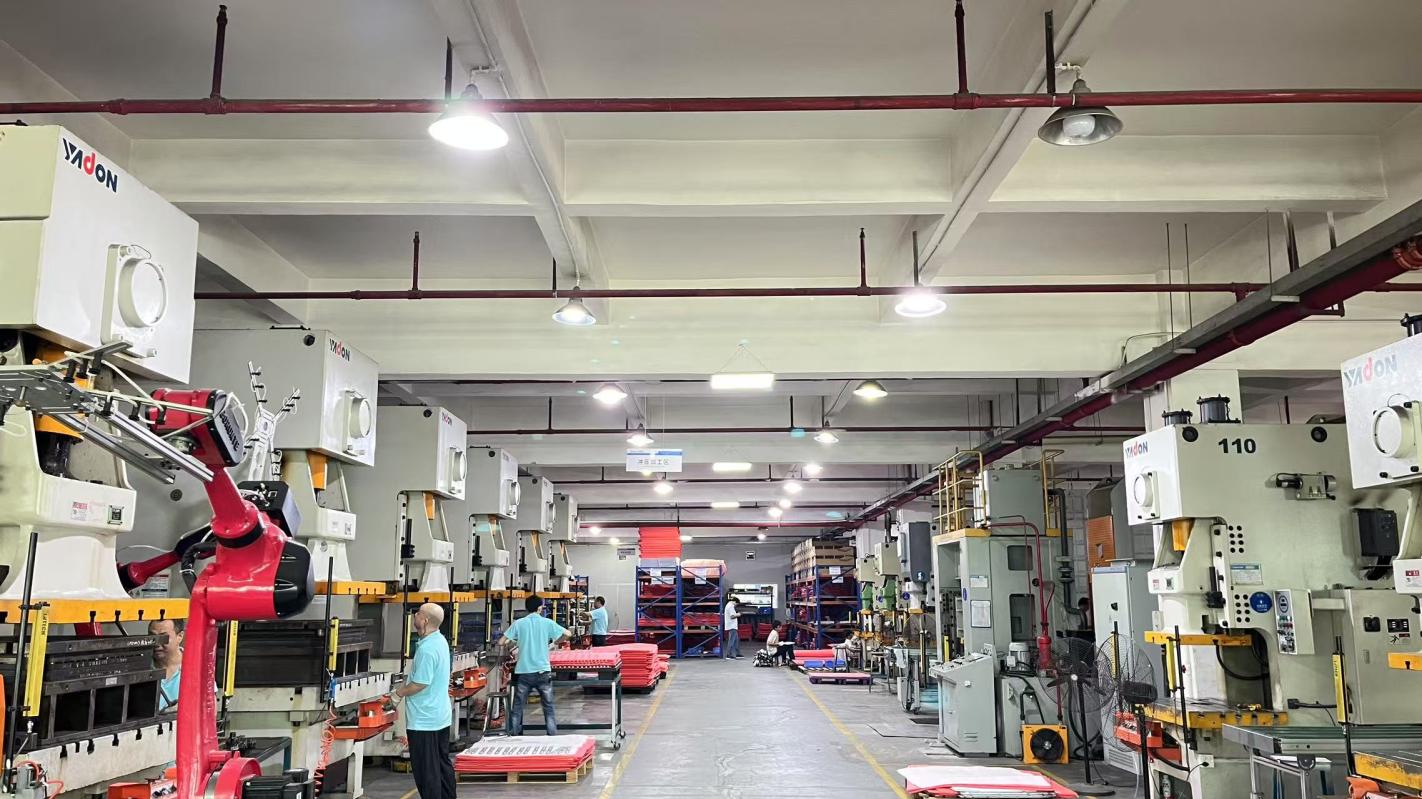
Industrial fans are not standalone equipment; they must adapt to localized environmental conditions and system requirements:
Data centers generate significant heat and operate continuously. Cooling systems must be reliable and energy-efficient. Intelligent exhaust arrays use variable-speed fans controlled by custom PCBA systems. Integrating high-density memory modules, such as Server DDR4 RAM, helps controllers manage real-time temperature data and dynamically adjust cooling to optimize energy use.
In environments with high dust, chemical vapors, and high temperatures, control electronics require robust physical protection. Component manufacturers address this by using technologies like double-layer HASL lead-free PCBs with protective conformal coatings. These boards are designed to handle high mechanical stress and thermal variations, providing stable operation in challenging settings.
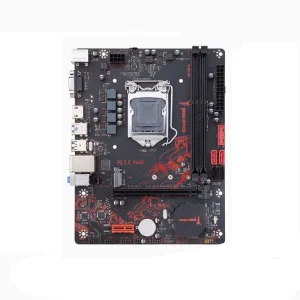
Large warehouses often use High-Volume Low-Speed (HVLS) fans to maintain air quality and manage humidity. To coordinate multiple units, facilities use centralized controllers like the Mini ITX N100 Motherboard. These micro-servers run management software to monitor air quality, adjust fan speeds, and maintain stable environmental conditions across the facility.
Answers to common questions about industrial ventilation, electronic controls, and customization options.
 Vorynex