Memory module manufacturing process turns individual memory chips into a tested, compatible component for computers, servers, and other devices. It is more than mounting chips on a circuit board. The work also involves materials control, precision assembly, firmware data, and electrical verification. Small details matter.
The industry’s scale is substantial. The Semiconductor Industry Association, drawing on WSTS data, reported global semiconductor sales of $627.6 billion in 2024, up 19.1% from 2023. That figure covers the wider semiconductor market, not memory modules alone, but it shows the scale of the ecosystem supplying their components. In practice, module makers source DRAM chips and printed circuit boards, then use surface-mount equipment to place components with tight alignment. DDR5 modules may also include an on-module power-management integrated circuit. Reflow soldering fixes the parts in place; optical inspection and electrical tests help identify defects.
This guide follows the process from incoming inspection through assembly, programming, and final testing. JEDEC standards help define module interfaces and specifications, while manufacturers set detailed production controls and acceptance limits. That distinction is easy to miss. A process can vary by module type, factory, and customer requirements. Factory reality is less tidy than a simple flowchart. We will also examine how solder quality, electrostatic-discharge controls, and test coverage affect reliability—and where a successful test still cannot guarantee every module will perform identically over its full service life.
Memory module design begins with the system’s workload, not a speed label. A compact industrial controller may need stable operation across temperature changes, while a workstation may prioritize capacity and bandwidth. Fit comes first. Designers match DRAM type, module capacity, rank, and data width to the host controller. JEDEC’s DDR5 SDRAM standard includes data rates up to 6,400 MT/s. That number is a reference point, not a promise that every board will run reliably at that speed. PCB routing, signal integrity, firmware support, and thermal conditions all matter. A small mismatch can cause intermittent errors that are difficult to reproduce.
Component selection also means checking the supporting parts. DDR5 modules use a power-management integrated circuit, and some designs add error-correction features for specific workloads. The PCB stack-up and trace lengths should be reviewed alongside the selected memory devices; a fast component cannot fix weak routing. One assumption worth challenging: the highest-rated speed is not automatically the best choice. TrendForce’s Q4 2024 outlook forecast conventional DRAM contract prices to rise 8–13% quarter over quarter, underscoring how sourcing costs can shift. Teams should compare availability, qualification needs, and lifecycle supply before locking a design. That trade-off is easy to underestimate.
Illustrative bill of materials for a non-ECC, single-rank x8 DDR5 UDIMM. The DRAM devices provide the module’s 64-bit data width; the PMIC and SPD hub support power management and module configuration.
For a memory module, PCB fabrication starts with the stack-up: thin copper layers bonded to a stable insulating core. The layout must preserve signal paths while leaving space for memory chips, power connections, and mounting points. Fabricators image and etch the copper, drill vias, then plate holes to connect layers. Small defects matter. A weak via can interrupt a signal or power path.
Preparation continues after the board takes shape. The manufacturer applies solder mask, adds a surface finish, and checks hole position, copper width, and board thickness. IPC-6012 and IPC-A-600 provide industry criteria for rigid-board performance and visual acceptability. These checks are useful, but they cannot replace testing against the module’s actual design. A board may pass visual inspection and still need electrical verification.
The production scale makes consistent preparation essential. Prismark’s 2023 PCB industry review estimated global PCB production value at about US$73.6 billion, reflecting the breadth of this manufacturing sector. For memory-module boards, fabrication records should track materials, process settings, and inspection results. Clean panels help, too. Dust or handling marks can compromise later assembly. One practical limitation: even a carefully controlled process can reveal design weaknesses only after prototypes are tested.
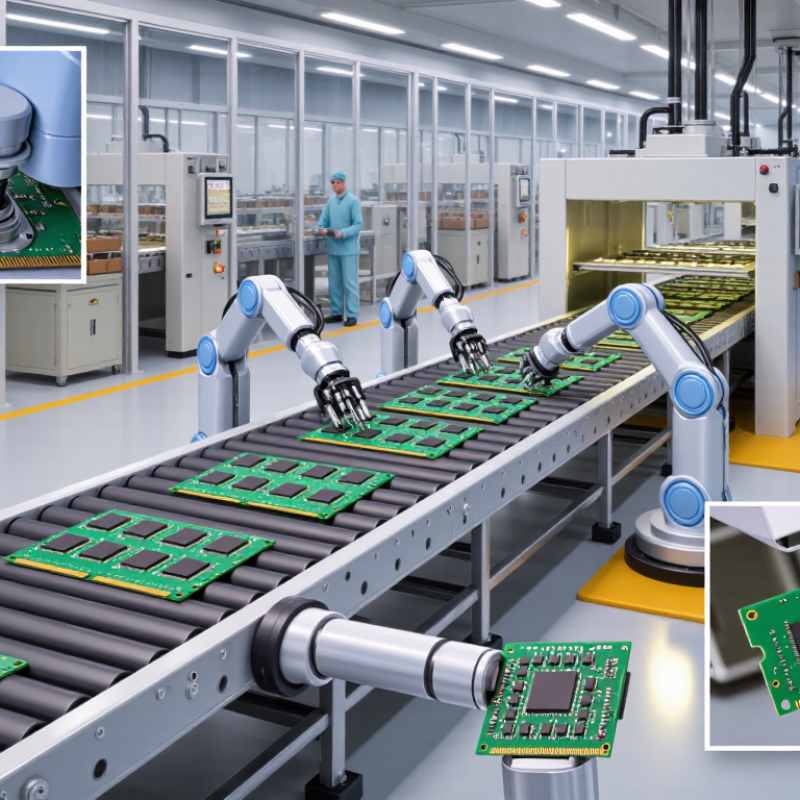
Memory module assembly depends on accurate component placement before soldering. The printed circuit board receives a controlled layer of solder paste through a stencil. Automated pick-and-place equipment positions memory chips and supporting components onto the paste. Small shifts matter. A chip placed slightly off its pads may form weak or uneven joints.
The board then passes through a reflow oven, where a staged temperature profile melts the paste and bonds each component. Heating too quickly can stress parts; insufficient heat may leave solder joints incomplete. Technicians check placement, polarity, and solder quality with optical inspection and, when needed, X-ray imaging. Not every defect shines. A board can look tidy while a hidden joint remains unreliable.
Tips: Keep boards dry and protected from static during handling. Verify paste condition and stencil alignment before each run. Watch the temperature profile, not just the oven’s displayed peak. If inspection finds repeated defects, review the process data before changing several settings at once. That discipline takes time, and it is easy to overlook a small placement drift during a busy production shift.
Memory modules face electrical, functional, and thermal checks before shipment. Testers verify capacity, transfer speed, SPD data, and signal integrity. A technician may watch a test screen flag a single failing address among millions. Small faults matter.
JEDEC test methods help standardize stress and environmental checks. However, laboratory passes cannot predict every field condition. A 2009 ACM SIGMETRICS study by Schroeder, Pinheiro, and Weber found that roughly 8% of observed DIMMs experienced errors annually. The finding supports screening, not a claim that every module will fail. Burn-in testing can expose weak cells under sustained load, while temperature cycling reveals sensitivity to heat. Inspectors also review solder joints, connector edges, and module labels under magnification. A clean appearance is not proof of reliability. That part is easy to overlook. Final sampling should retain test logs, failure codes, and lot details, so engineers can trace recurring issues. No inspection catches everything, and test limits deserve regular review.
After electrical testing, each memory module needs an identity that stays readable through packing and shipment. A label may carry a part number, capacity, speed grade, serial number, and production lot. The exact fields depend on the product and customer requirements. Operators compare printed data with the build record before applying it. Scanners then verify that the code resolves to the correct unit. A smudged barcode can slow receiving, even when the module itself works perfectly. Small details matter. Labels should avoid contacts and components while remaining visible after installation. Placement can vary slightly across module designs, so fixtures and visual checks help reduce mistakes.
Packaging protects both the circuitry and the information attached to it. Modules are commonly placed in antistatic trays or carrier tape, then sealed in moisture-barrier bags when needed. Desiccant and humidity indicator cards provide useful evidence of package condition. The sealed packs go into cartons with cushioning that limits movement during transit. Before release, staff reconcile carton quantities, lot identifiers, and shipping documents. Errors happen. A mismatch may come from a reprint or counting error, and should be checked rather than casually corrected. Distribution teams track storage conditions, shipment scans, and handoffs to the receiving site. Clear records help investigate a damaged seal or missing carton, though careful handling remains easy to underestimate.
| Process Stage | Activity | Typical Data and Records | Handling or Quality Control |
|---|---|---|---|
| 1. Final Inspection | Completed memory modules are checked against product specifications. Inspections may include visual examination and electrical or functional testing. | Product configuration, test status, inspection result, production lot, and traceability records. | Only modules meeting the applicable acceptance criteria proceed to packing. Nonconforming units are identified and kept separate. |
| 2. Product Identification | A label is applied to the module or its carrier, as appropriate for the product design and handling method. | Part or item number, capacity, module type, serial or lot identifier, and other product-specific identification. | Label information is checked for legibility and matched to the product and its production records. |
| 3. Barcode and Traceability | Identification may be encoded in a barcode or other machine-readable format to support inventory and shipment tracking. | Encoded item or lot details, quantity, and applicable date or production codes. | Scans or verification checks help confirm that printed and encoded information agrees with the packing records. |
| 4. ESD-Safe Packing | Modules are placed in suitable protective packaging, such as an electrostatic-discharge (ESD) protective bag, tray, or carrier. | Pack configuration, quantity per package, and package or lot identification. | Packaging is selected to reduce electrostatic and physical damage risks during storage and handling. |
| 5. Moisture and Physical Protection | Where required by the product and shipping conditions, additional moisture-barrier packaging and cushioning are used. | Packaging type and any applicable moisture-control or handling information. | Packaging requirements depend on the product specification. Seals and protective materials are checked before closure. |
| 6. Carton Packing | Individual packs or trays are consolidated into shipping cartons and secured for transport. | Item identification, total quantity, lot details, carton identification, and destination information. | Carton contents are reconciled with packing records; cartons are closed and labeled for handling and shipment. |
| 7. Warehouse Receipt and Storage | Packed goods are recorded into inventory and stored until order allocation or dispatch. | Receipt date, location, quantity, lot or serial references, and inventory status. | Inventory systems support traceability and stock rotation. Packages are stored under conditions appropriate to their specifications. |
| 8. Order Picking and Verification | Products are selected for an order, and the picked items are checked against the order and shipment documentation. | Order reference, item number, quantity, lot or serial references, and destination. | Scanning or other verification helps prevent quantity, identification, and destination mismatches. |
| 9. Dispatch and Distribution | Cartons are prepared for carrier handoff and transported through the distribution network to the receiving location. | Packing list, shipping label, shipment reference, carrier details, and tracking information where available. | Outer packaging is checked for closure and visible damage. Shipment records support delivery tracking and downstream traceability. |
Label content, packaging methods, and inspection requirements vary by product specification, customer requirements, and applicable handling standards.
Start with the system’s workload. A compact controller may need stable operation across temperature changes, while a workstation may need more capacity and bandwidth.
No. A rated speed is only a reference. Board routing, firmware support, signal quality, and heat can limit reliable operation.
Match the memory type, capacity, rank, and data width to the host controller. Also review the power-management chip, PCB layers, and trace lengths.
Compare availability, qualification needs, and expected supply life before fixing a design. Prices can shift, so the cheapest choice today may cause trouble later.
Tests can verify capacity, transfer speed, stored module data, and signal quality. A test screen may flag one faulty address among millions. Small faults matter.
Burn-in can expose weak cells during sustained operation. Temperature cycling can reveal sensitivity to heat. Neither test covers every field condition.
Inspect solder joints, connector edges, and labels under magnification. A clean surface is not proof of reliability. That is easy to overlook.
No. One study reported errors in roughly 8% of observed modules annually, not in every module. Keep test logs and review limits; some issues may still escape detection.
The Memory module manufacturing process begins with careful design and component selection. Engineers determine the module’s specifications, choose compatible memory chips and supporting components, and plan the circuit layout. A printed circuit board is then fabricated and prepared, with its electrical pathways and surfaces checked to ensure it is ready for assembly.
Memory chips and other components are placed on the board and soldered using controlled production methods. Each assembled module undergoes functional testing and quality inspection to check performance, reliability, and conformity with its intended specifications. Once approved, the modules are labeled, packaged to protect them during handling and transport, and prepared for distribution. These stages work together to produce consistent memory modules ready for use in compatible systems.
Vorynex